If you’ve ever walked the floor of a commercial electrical manufacturing plant, you’ve likely been in awe of the precise, heavy-duty parts that go into powering everything from skyscraper HVAC systems to data center cooling infrastructure. At the center of many of these parts is a busbar—a rigid, conductive metal bar used to distribute electrical current across panels, switchgear, and distribution units. For those of us who supply busbar processing machines, one question comes up at least once a week, often from new electrical contractors or small-scale component makers still learning the ins and outs of their trade: “What is the minimum bending radius of a busbar processing machine?” Busbar Processing Machine
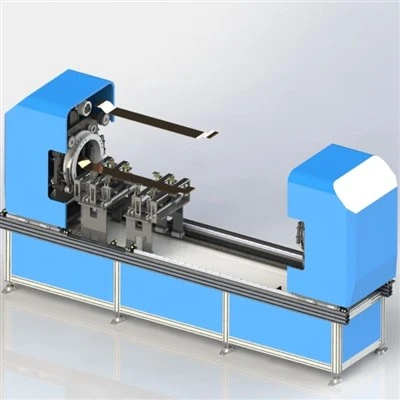
It’s a deceptively simple question, but the answer isn’t a one-size-fits-all number. Over the 12 years I’ve spent working with manufacturers, troubleshooting machine setups, and helping customers adjust their projects to fit their equipment, I’ve learned that this minimum bending radius is a critical specification that balances material science, machine capability, and the actual needs of a job. Let’s break this down, starting with what the minimum bending radius even means, how it’s calculated, what impacts it, and what that means for anyone looking to purchase or operate a busbar processing machine.
First, let’s define the basics. The minimum bending radius (often shortened to MBR) of a busbar processing machine is the smallest radius a machine can bend a busbar without causing permanent damage to the metal—damage that can ruin the part, create hot spots, or even cause electrical failure down the line. That damage comes in a few forms: cracking along the outer edge of the bend, thinning of the metal’s cross-section which reduces its conductivity, or distortion of the internal grain structure of the metal that weakens it over time. When I first started in this industry, I had a customer who tried to bend a 10mm thick copper busbar with a machine rated for a 50mm MBR, using a 30mm radius tool. The part looked fine at first, but when they ran a full load test a week later, the bend cracked and caused a full panel shutdown. That’s the kind of mistake that makes even experienced operators double-check their numbers.
Now, how is this MBR determined? It’s not arbitrary set by machine manufacturers (though we do publish a rated MBR for each machine line). The core formula for minimum bending radius comes from material science research, specifically the relationship between the material’s thickness and its ductility—the ability to bend without breaking. The most common busbar materials are copper (99.9% pure, the standard for most electrical applications) and aluminum, with copper being more ductile and easier to bend than aluminum, which is stiffer and more prone to cracking.
The general industry rule of thumb that most new operators learn is this: MBR = (k × t), where t is the thickness of the busbar, and k is a constant that depends on the material. For pure copper, k is typically between 3 and 5, which means a 10mm thick copper busbar would have an MBR of 30mm to 50mm. For aluminum, that k jumps to 6 to 8, so the same 10mm thick aluminum bar would need an MBR of 60mm to 80mm. That’s a big difference, and it’s one of the first things I walk new customers through when they’re reviewing machine specs.
But here’s where it gets complicated, and where I’ve seen a lot of misinformation online: that formula is a baseline, not a hard limit. The MBR also depends on three other key factors: the width of the busbar, the type of bend (90-degree, U-bend, multi-radius), and the specific design of the machine itself. Let’s talk about machine design first, since that’s the part I know best as a supplier.
Not all busbar processing machines are created equal. A manual, compact machine for small job shops will have a much larger MBR range than a fully automated, hydraulic machine for high-volume industrial production. For example, our entry-level manual bending machines, designed for small electrical contractors who do custom panel builds, have a minimum bending radius of 75mm for copper busbars up to 6mm thick. Our mid-range hydraulic machines, used by component manufacturers producing 10,000+ parts a year, have an MBR as low as 25mm for copper up to 12mm thick. Our top-of-the-line fully automated machines, which can handle multi-busbar setups and precision bends for data centers, have a minimum MBR of just 15mm for thin copper busbars under 5mm thick.
Why such a big range? It comes down to the machine’s components: the bending die (the tool that forms the radius), the pressure of the bending ram, and the control system that adjusts for material thickness. Lower-end machines use generic bending dies that are only available in standard sizes, so you can’t get a tight radius without forcing the metal. Higher-end machines have custom, precision-machined dies that match the exact thickness of the busbar, and hydraulic pressure that can be adjusted in real time to avoid over-bending or stretching the metal. I’ve had customers upgrade from entry-level to mid-range machines specifically because they needed to bend smaller-radius parts for solar panel mounting busbars, which use thinner copper but require tight bends to fit in the limited space of a solar inverter.
Next, the width of the busbar. The formula I mentioned earlier uses thickness, but width matters too. A 10mm thick copper busbar that’s 50mm wide will have a different MBR than the same thickness bar that’s 100mm wide. Wider bars have more surface area along the bend, so the stress is distributed differently. For wider bars (over 50mm), we typically adjust the k factor to be higher—around 5 to 6 for copper, instead of 3 to 4. I learned this the hard way about 8 years ago, when a customer was bending 100mm wide, 8mm thick copper busbars for a subway power distribution system. They tried using the standard 40mm MBR for their thickness, and the bend would buckle along the width because the wider bar couldn’t handle the tight radius. Once we adjusted the MBR to 50mm, the bends came out perfect, and the part passed all electrical safety tests. That experience taught me to always ask for both thickness and width when a customer is asking about MBR—width is just as important as thickness.
Then there’s the type of bend. A simple 90-degree bend in a single flat plane has a consistent MBR, but when you’re doing a U-bend, a multi-plane bend, or a bend with multiple bends along the same bar, the MBR requirements change. For example, a U-bend has two 90-degree bends facing each other, so the space between them has to be large enough to accommodate the MBR of both bends plus the space required for the bar itself. I recently had a customer working on a switchgear panel that needed a U-bend with the two bends only 150mm apart. If they used a 40mm MBR for their 10mm thick copper, that would leave just 10mm between the two bends, which was too small for their panel design. We worked with them to adjust their part design slightly, or upgrade to a machine that can do a slightly smaller MBR (30mm) for their thickness, which freed up enough space. It’s a trade-off, but it’s one that comes up all the time.
Now, let’s talk about common mistakes I see customers make when working with busbar MBR. The first is trying to use a machine’s general spec as a one-size-fits-all number, without accounting for their specific material thickness, width, and bend type. A customer will come to us and say, “I need a machine with a 20mm MBR,” not realizing that spec is only for thin, narrow busbars. If they need to bend a thick, wide bar, that 20mm spec is impossible, and they’ll end up with ruined parts. The second mistake is ignoring material temper. Copper comes in different tempers: soft (annealed) copper is much more ductile than hard copper (hard-temper). Annealed copper can have an MBR that’s 20-30% smaller than hard copper of the same thickness, because it’s easier to bend without cracking. I always recommend customers use annealed copper for tight-radius bends, even if it costs a little more upfront—it saves money on ruined parts and rework in the long run.
Another point that’s often overlooked is compliance with electrical safety standards. Busbars are used in high-voltage applications, so the quality of the bend directly impacts safety. The International Electrotechnical Commission (IEC) has standards for busbar bending, and the National Electrical Manufacturers Association (NEMA) in the US has its own guidelines. For example, NEMA PB-2, which covers power busways, specifies that any bend must not reduce the cross-sectional area of the busbar by more than 5%, and that cracks or crevices in the bend are not allowed. If a bend is made with a radius smaller than the MBR, the cross-sectional area is reduced, which increases electrical resistance and can cause overheating—a major safety hazard. That’s why the MBR isn’t just a machine capability; it’s a critical part of meeting industry standards and building safe, reliable electrical equipment.
So, how do you choose the right minimum bending radius for your project and your machine? Let’s walk through a step-by-step process that I share with every customer, because it works every time. First, note the material: copper or aluminum, and its temper (annealed or hard). Second, measure the thickness and width of the busbar you’ll be working with. Third, figure out the type of bend (90-degree, U-bend, multi-plane) and any space constraints for the part. Fourth, apply the basic formula, adjusting for width and bend type: MBR = (k × t), where k is 3-5 for thin/narrow copper, 5-6 for wide copper, 6-8 for thin/narrow aluminum, and 8-10 for wide aluminum. Fifth, check your machine’s rated MBR for that thickness and material, and if it doesn’t meet your requirement, decide if you need to adjust your part design, switch to annealed material, or upgrade to a machine with a smaller MBR.
Over the years, I’ve had customers come to me thinking that a smaller MBR is always better, because it saves space. But space isn’t the only consideration. If a tight radius requires forcing the metal, you end up with a weaker part that’s more likely to fail. I had a customer who designed a panel with busbars bent to an MBR that was too small, and within two years, three of the bends had cracked due to thermal cycling—when the busbar heats up and cools down as power is turned on and off, the stress from the tight bend causes the metal to fatigue. That ended up being a much more expensive fix than if they had slightly larger bends. The key is balance: get the smallest MBR that works for your part design and machine, without sacrificing material integrity or safety.
If you’re in the market for a new busbar processing machine, don’t just look at the published MBR number on the spec sheet. Ask the supplier for the MBR for the exact material thickness, width, and bend type you work with. A reputable supplier will be able to give you specific numbers, not just a general range, and explain how the machine’s design enables that radius. For example, when a customer asks me, “Can your machine bend a 10mm thick, 80mm wide annealed copper bar to a 35mm MBR?” I don’t just say yes or no—I’ll tell them that yes, our mid-range hydraulic machine can do that, because of the precision-machined bending die and adjustable pressure, and I can even share photos of parts we’ve made with that exact setup.
For existing machine owners who are struggling with bending parts that crack or don’t meet their design requirements, the fix might not be a new machine. It could be switching to annealed material, adjusting the bending pressure to reduce stress on the metal, or upgrading your bending dies to ones that are custom-sized for your material thickness. I’ve spent countless hours on the phone with operators walking them through these adjustments, and 70% of the time, the problem is not the machine’s MBR, but a small tweak in setup or material choice.
At the end of the day, the minimum bending radius of a busbar processing machine is more than just a technical spec. It’s a reflection of how well the machine is designed to balance material science, precision, and real-world application needs. As a supplier, our job is to not just sell a machine with a good MBR, but to help each customer understand what MBR they actually need for their specific work, so they can make parts that are safe, reliable, and fit their project requirements. If you’re working on a new project, troubleshooting a bend that’s not working, or looking to upgrade your busbar processing equipment, I’m here to help you sort through the details. Don’t hesitate to reach out to discuss your specific needs and find the right solution for your business.
Busbar Processing Machine References:
- International Electrotechnical Commission (IEC) 61439: Low-voltage switchgear and controlgear assemblies, 2020.
- National Electrical Manufacturers Association (NEMA) PB-2: Power Busways, 2018.
- Copper Development Association (CDA): Copper Busbar Bending Guidelines, 2021.
- Aluminum Association: Aluminum Electrical Conductor Handbook, 7th Edition, 2019.
Suzhou Kiande Electric Co., Ltd.
Suzhou Kiande Electric Co., Ltd. is one of the most professional busbar processing machine manufacturers and suppliers in China, also supports custom service and OEM&ODM service. Welcome to buy durable busbar processing machine made in China here and get quotation from our factory. Quality products and reasonable price are available.
Address: No.123, Suzhou Avenue East, Suzhou Industrial Park Suzhou, Jiangsu 215000 China
E-mail: saleswmkc@kiande.cn
WebSite: https://www.busbarcncmachine.com/
